Phone Case Screen Printing | LED UV Curing Lamp Retrofit of Automatic Screen Printing Line Solves Thin-Case High-Temperature Deformation and Ink Adhesion Problems
News 2026-11-20
Project Information
| Item | Details |
| Contact Person | Manager Liu |
| Factory Address | Shenzhen, Guangdong, China |
| Company Type | UV ink screen printing factory for consumer electronics housings |
| Number of Employees | About 200 people |
| Main Products | UV ink screen printing on plastic/composite phone cases |
| Downstream End Customers | Domestic phone brands, smart wearable device brands, phone solution providers |
| Core Process Involved | Automatic screen printing → UV curing → Cooling and unloading → Cross-hatch / abrasion inspection |
| Ink Used | UV screen printing ink (wear-resistant type), light absorption peak in the 395nm UVA band |
| Printing Substrates | PC injection-molded parts, PC+ABS composite sheet, TPU soft cases, glass-fiber reinforced composite |
| Curing Equipment Before Retrofit | Conventional high-pressure mercury lamp UV curing machine |
| Production Line Configuration | Automatic screen printing line + tunnel curing furnace, multiple parts arranged side by side |
| Line Speed Before Retrofit | 4 m/min |
| Target Line Speed | ≥7 m/min |
| Workshop Conditions | Constant temperature 23±2℃; cleanroom class 1,000 in the screen printing workshop |
| Core Pain Points Before Retrofit | 1. Phone cases are thin-walled (0.6~0.8mm); mercury lamp heat radiation deforms the case 2. Light-colored cases turn yellow at high temperature, causing appearance defects 3. Ink at curved edges and corners is under-cured; abrasion tests fail and printed patterns/ink peel off 4. Long mercury lamp warm-up, short tube life, frequent shutdowns for replacement 5. Strong ozone odor; exhaust system runs continuously at high load |
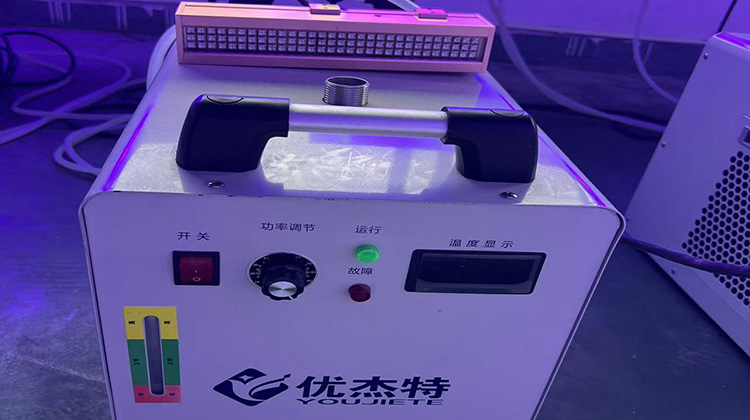
| Selected Equipment Model | YJT-CT4-400A water-cooled LED UV curing lamp, tunnel type |
| Working Wavelength | 395 nm |
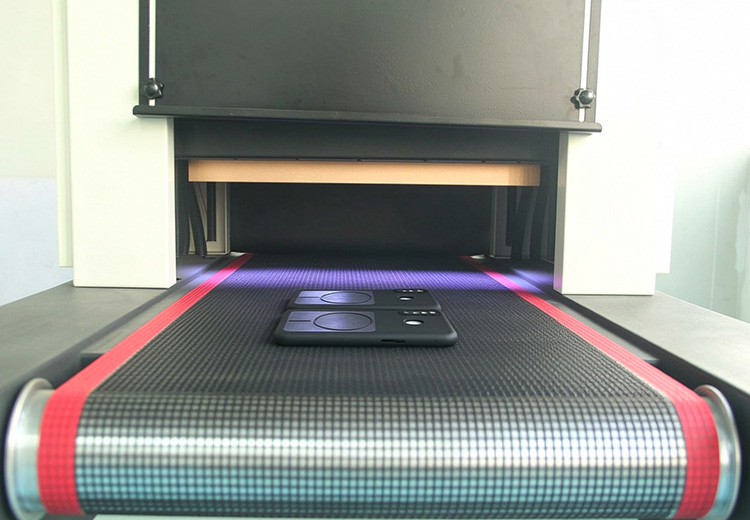
| Installation Method | Inline type; installed after the printing leveling station; customized emitting surface adapted to multiple parts arranged side by side |
| Customer Acceptance Criteria | 1. Thin-wall cases free of deformation and yellowing 2. Screen printing ink fully cured at curved edges and corners; cross-hatch adhesion 4B or above 3. RCA abrasion test ≥200 cycles without exposing the substrate 4. Instant on, no warm-up required 5. No ozone generated |
| Reliability Test Standards | ASTM D3359 cross-hatch adhesion; RCA paper tape abrasion test; 90℃ high-temperature high-humidity 48h aging; artificial sweat corrosion resistance test |
| Project Timeline | Sample proofing confirmation: 5 working days (including multi-angle curved surface verification) Equipment delivery + on-site installation and commissioning: 10 working days |
| Expected Benefits for the Customer | Lower case deformation and ink abrasion defect rate, improved mass production yield, savings on tube consumables and electricity, and an improved workshop environment |
1. Project Background
The customer is located in Shenzhen, Guangdong, with Manager Liu as the contact person. The factory has about 200 employees and specializes in providing automatic UV ink screen printing services for phone cases to domestic phone brands and smart wearable device solution providers. As a global center of the consumer electronics industry, Shenzhen is surrounded by a large number of phone whole-machine solution providers and OEM factories, so demand for appearance screen printing is strong and quality requirements are stringent. The customer operates several semi-automatic screen printing lines, printing UV ink on PC injection-molded parts, PC+ABS composite sheet, TPU soft cases, and glass-fiber reinforced composite housings; products include phone back covers, middle frames, and smart watch shells.
Before the retrofit, the curing equipment on the line was a conventional high-pressure mercury lamp. The phone case wall is only 0.6~0.8mm thick and extremely temperature-sensitive; the large amount of infrared heat radiation from the mercury lamp caused slight warping and deformation after the cases passed through, and flatness fell out of tolerance. Light-colored (white, silver, beige) cases yellowed after high-temperature baking, color difference exceeded limits, and the appearance defect rate stayed high. Phone cases have a curved structure; under the broad-spectrum mercury lamp, light intensity attenuates noticeably at curved edges and corners, leaving the ink in those areas under-cured — cross-hatch adhesion was only grade 1~2, and the RCA paper tape abrasion test exposed the substrate in fewer than 80 cycles, leading to frequent returns and complaints. In addition, the mercury lamp required 5~10 minutes of warm-up, and the tube needed replacement after about 800~1000 hours of decay; frequent shutdowns for tube replacement caused capacity losses. The ozone odor was strong, and the exhaust system of the class-1,000 cleanroom ran at high load year-round, with high energy cost. The customer urgently needed a low-temperature curing solution with even, stable light intensity to improve mass production yield.
2. Solution Selection
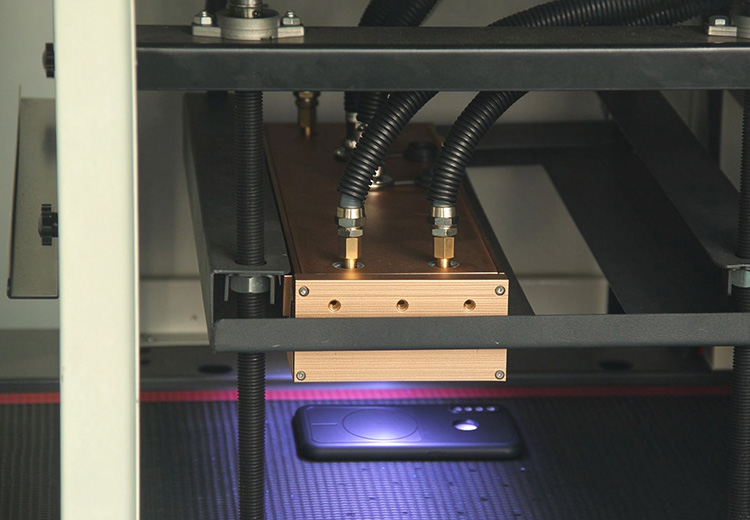
Our engineers visited the customer’s automatic screen printing line in Shenzhen for an on-site survey. Taking into account the thin-wall structure of the phone case, the curved arrangement, the absorption curve of the UV screen printing ink formulation, and the line speed, we recommended a water-cooled LED UV curing lamp. The 395nm wavelength was chosen to precisely match the photoinitiator absorption peak of the plant’s wear-resistant UV screen printing ink. According to the side-by-side arrangement of workpieces on the line, the emitting surface was custom-made to ensure even intensity coverage at every angle of the curved case with no dark areas at the edges; UV energy is continuously adjustable from 0~100%, with a 30% power margin reserved for curing dark and thick-ink-layer screen printing inks. Water cooling keeps light intensity stable without decay during long continuous production; the cold light source keeps workpiece temperature rise within 15℃, protecting thin-wall cases from deformation and yellowing.
3. Proofing Tests and Comparative Data
During the preliminary free proofing stage, side-by-side comparison tests were conducted on site using the same PC+ABS cases (0.7mm wall thickness), the same UV screen printing ink color group, and the same workshop conditions, focusing on ink curing at curved edges, case temperature rise, and abrasion performance. The test results are shown in the table below:
| Test Item | Unit | Mercury Lamp | YJT-CT4-400A Water-Cooled LED UV Curing Lamp, Tunnel Type | Test Basis |
| Rated Power | W | 400 | 2400 | Product Specification |
| Peak Energy | mW/cm² | 350~420 | 12000~20000 | Measured with UV radiometer |
| Working Distance | mm | 150~200 | 60~90 | Production Setting |
| Curing Time | s | 20~30 | 4~6 | Appearance + non-tacky check |
| Warm-up Waiting Time | s | 300~600 | 0 (instant on) | On-site production line record |
| Energy Required for Full Curing | mJ/cm² | 800~900 | 350~420 | Measured with UV radiometer |
| Cross-Hatch Adhesion | Grade | 1~2B | 4B~5B | ASTM D3359 |
| RCA Paper Tape Abrasion | cycles | 60~100 | 220~280 | RCA paper tape abrasion tester |
| Case Flatness Deformation | mm | 0.15~0.25 | 0.02~0.05 | 2D vision measurement |
| Yellowness Δb of Light-Colored Cases | — | 2.5~3.2 | 0.3~0.6 | Colorimeter measurement |
| Curing Uniformity at Curved Edges | — | Edge energy attenuation 40%+ | Edge energy attenuation <8% | Multi-point UV radiometer measurement |
| Overall Screen Printing Defect Rate | % | 6.8~9.5 | 0.8~1.2 | Statistics over 10,000 consecutive parts |
| Case Surface Temperature | ℃ | 75~90 | 35~40 | Infrared thermometer |
4. Implementation and Project Results
After proofing verified ink curing at curved edges, case temperature rise, and ink adhesion and abrasion performance, the solution was confirmed and the lamp head was custom-produced. After delivery, our technicians installed and wired the equipment on site, and commissioned it; we also trained operators on equipment operation as well as daily maintenance of the water circuit and lamp surface. The complete unit comes with a two-year warranty, and after-sales engineers respond quickly to urgent production line issues.
The following results were achieved after entering mass production:
1. Cold-light low-temperature curing leaves 0.6~0.8mm thin-wall PC/PC+ABS cases free of warping and deformation; flatness deformation dropped from 0.15~0.25mm to 0.02~0.05mm;
2. Yellowness Δb of light-colored cases dropped from 2.5~3.2 to 0.3~0.6, and the color-difference pass rate improved significantly;
3. Light intensity is even across 3D curved edges; edge energy attenuation dropped from 40%+ to within 8%, cross-hatch adhesion improved from 1~2B to 4B~5B, and RCA abrasion improved from 60~100 cycles to 220~280 cycles;
4. The light comes on instantly with no warm-up required, suiting continuous automatic screen printing; line speed increased from 4 m/min to 8 m/min;
5. The overall screen printing defect rate dropped from 6.8%~9.5% to 0.8%~1.2%; based on a monthly output of 500,000 cases, about 30,000 fewer defective pieces are produced each month;
6. Compared with the traditional mercury lamp, it saves about 75% of electricity; the light source lasts 20000~30000 hours, greatly reducing tube replacement and downtime capacity losses;
7. No ozone is generated, there is no pungent odor in the workshop, and the exhaust load on the class-1,000 cleanroom is significantly reduced.
If your production line also suffers from thin-part deformation, unstable ink adhesion, or heat damage, please feel free to contact us. We accept sample curing tests and provide test reports with measured data. Custom fixtures and energy adjustment services are available.